

Expert Insight: Staircase stringers for high-end custom manufacturing require precision above everything else. For instance, choosing the right cutting technology directly impacts structural integrity and aesthetic finish. However, deciding between CNC laser cutting and plasma cutting can be challenging for fabricators. As a result, understanding their core differences is essential.
On the one hand, CNC laser cutting offers exceptional accuracy and a smoother edge finish, making it ideal for intricate designs and thinner metals. Moreover, the heat-affected zone is minimal, which prevents warping. On the other hand, plasma cutting excels in handling thicker plates efficiently and at a lower operational cost. Consequently, your choice ultimately depends on your specific production volume, material thickness, and budget requirements.
In my 9 years at Meizstairs, I’ve seen shops invest in the wrong cutting technology because they focused only on precision, not on the material thickness range they actually process. For straight stairs stringers cut from 5mm plate, fiber laser cutting is hard to beat. But for heavy-duty stringers from 16mm+ steel, plasma cutting delivers faster speeds and lower operating costs.”
Du fournisseur de produits au partenaire de résolution de problèmes
Practical comparisons of CNC laser cutting and plasma cutting are essential for high-volume staircase stringers production. Furthermore, experts at Meizstairs believe that selecting the right cutting technology is just as critical as choosing the correct steel grade.
| Diagnostic fondé sur l'expérience | Approche globale | Partenariat à long terme |
|---|---|---|
| 15 years of production data help us identify why certain steel stair fabrication projects struggle (wrong consumable costs, excessive post-processing). | We consider your material thickness range, production volume, and quality requirements to recommend the optimal fabrication solution. | Your staircase’s quality and cost-efficiency are our success. We’re committed to delivering the right fabrication solution. |
Understanding Cutting Technologies for Staircase Stringers
When fabricating custom staircase stringers, selecting the appropriate thermal cutting method is crucial. Furthermore, manufacturing efficiency heavily relies on understanding how these machines operate. Specifically, both options utilize thermal energy to slice through thick metals, yet they perform differently under industrial conditions. Consequently, fabricators must evaluate their specific operational needs before committing to a technology.
CNC Laser Cutting for Staircase Stringers
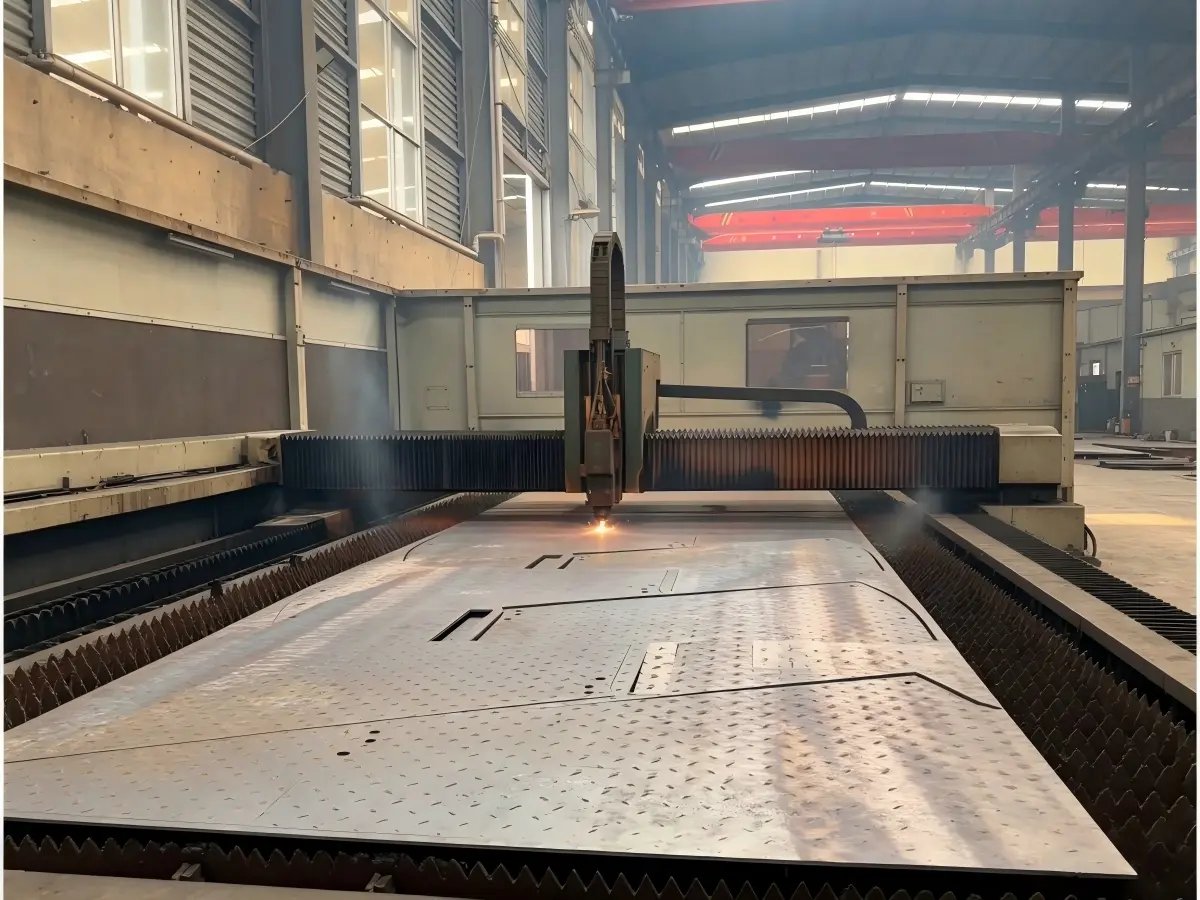
CNC laser cutting uses a focused beam to melt and vaporize material. The process works by directing high-powered light through optics, creating a concentrated heat source that cuts with exceptional precision.
How it works: The laser pulse generates intense heat that melts the metal, while an assist gas (oxygen or nitrogen) blows the molten material away. Fiber laser cutting—the most common type for metal fabrication—delivers the laser beam through fiber optic cables, offering high energy efficiency and cutting speeds on thin materials.
Plasma Cutting for Staircase Stringers
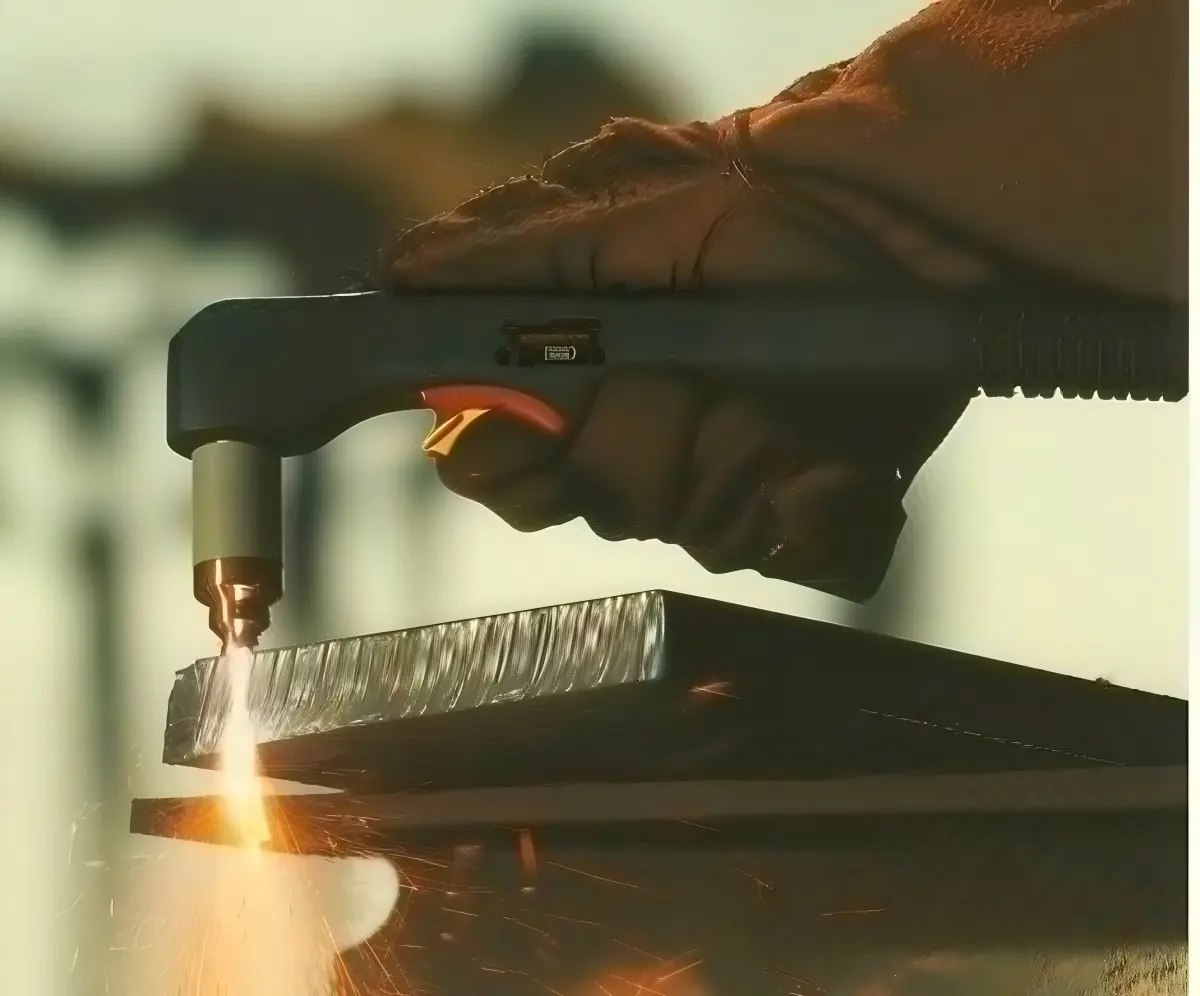
Plasma cutting (also called arc cutting) uses ionized gas—plasma—to cut electrically conductive metals. Specifically, a plasma cutting machine generates an electrical arc that superheats compressed gas (air, oxygen, or nitrogen), creating a plasma stream that melts the metal.
How it works: Through a specialized plasma cutting torch, this process directs a high-velocity plasma jet straight onto the workpiece. Specifically, the plasma arc relies on an active circuit where the plasma stream completes the electrical path through conductive material, thereby melting it in motion. Consequently, modern CNC plasma systems guide the torch along precise programmed paths to ensure repeatable, high-quality results.
Staircase Stringers: Laser vs Plasma Comparison
Now that we’ve examined both technologies, let’s compare them side by side across the dimensions that matter most for staircase stringers production.
Cutting Quality and Precision
| Parameter | CNC Laser Cutting | Plasma Cutting |
|---|---|---|
| Cutting accuracy | ±0.003″ to ±0.030″ | ±0.008″ to ±0.1″ |
| Kerf width | 0.004″-0.012″ (0.1-0.3mm) | 0.04″-0.08″ (1-2mm) |
| Edge quality | Smooth, burr-free, minimal slag | Good, but may require finishing |
| Heat-affected zone | Minimal (~0.1mm) | Larger (0.5-1mm) |
| Bevel / angularity | Near 90° | Slight bevel possible |
Furthermore, laser cutting delivers superior precision and edge quality—laser cutting sheet material results in clean edges that often require no finishing. Plasma cutting produces acceptable quality but typically leaves dross or a slightly rougher edge that may need grinding or deburring.
Speed and Thickness Capability
| Material Thickness | CNC Laser Cutting Speed | Plasma Cutting Speed |
|---|---|---|
| 5mm mild steel | 4.2-6 m/min (faster) | 2.3-2.6 m/min |
| 10mm mild steel | 1.8-2.3 m/min | 2.6-2.8 m/min (faster) |
| 16mm mild steel | Speed advantage disappears | Plasma achieves faster cutting |
| 20mm+ mild steel | Limited (≤25-30mm effective) | Excels (up to 50-75mm+) |
Moreover, for stair stringer production: If you’re cutting stringers from 5-6mm plate—common for straight stairs and home stairs—fiber laser cutting can be up to 5x faster than plasma. For heavy-duty stringers from 16mm+ steel—typical for commercial staircase and industrial applications—plasma cutting becomes faster and more cost-effective.
Material Compatibility
| Matériel | CNC Laser Cutting | Plasma Cutting |
|---|---|---|
| Mild steel | Excellent | Excellent |
| Stainless steel | Excellent | Good (lower quality) |
| Aluminum | Good (high-power required) | Bien |
| Copper / Brass | Challenging (reflective) | Bien |
| Rusted / painted steel | Requires cleaning or pre-cut pass | Cuts without issue |
| Non-conductive materials | Yes (wood, plastics) | No—only conductive metals |
Additionally, plasma cutting excels with imperfect materials—rust, paint, and scale don’t affect the process. In contrast, laser cutting requires clean surfaces for optimal results.
Cost Comparison for Staircase Stringers
| Cost Factor | CNC Laser Cutting | Plasma Cutting |
|---|---|---|
| Equipment cost | $250,000–$500,000+ | $50,000–$100,000 |
| Operating cost | ~$20/hr | ~$15/hr |
| Consumables | Fewer—longer life | Electrodes/nozzles require frequent replacement |
| Post-processing | Minimal | May require grinding/deburring |
Moreover, plasma cutting has a lower entry cost and is more economical for thicker materials. Laser cutting offers lower operating costs on thin materials due to higher speed and fewer consumables.
Applying Cutting Technology to Staircase Stringers
Based on these comparisons, here’s how to apply each technology to your production.
When to Choose CNC Laser Cutting
Best for:
- Thin plate stringers from 4-10mm steel plate (standard residential stairs, light commercial)
- High-precision parts with tight tolerances
- Straight-run stairs with repetitive patterns
- Large-batch production of thin components
- Materials that require clean edges with no post-processing
Typical stair types:
- For straight stairs, standard stringer profiles work well
- L-shaped designs benefit from precision notch cuts
- Mono stringer stairs need clean, visible edges
- Residential applications include home stairs
For high-end architectural metalwork, CNC laser cutting remains a top choice. In addition, it provides exceptional precision for intricate stringer designs and complex geometric patterns. Moreover, the narrow kerf width minimizes material waste, while the lower heat input reduces thermal distortion. Therefore, it is the ideal solution for projects demanding flawless visual aesthetics and tight tolerances.
When to Choose Plasma Cutting
Best for:
- Thick plate stringers from 12-25mm+ steel plate (heavy-duty commercial stairs, industrial applications)
- Heavy structural components where extreme precision is less critical
- Imperfect material conditions (rust, scale, paint present)
- Thick-section cutting where laser speed diminishes
- Budget-sensitive projects where lower capital investment is required
Typical stair types:
- For commercial staircases with heavy-duty stringers
- Industrial applications include stairs and platforms
- Outdoor installations use steel stairs with corrosion-resistant coatings
- Large-scale structural components for stair systems
On the other hand, plasma cutting offers unmatched advantages for heavy-duty production. For instance, it excels at slicing through thick structural steel plates at a significantly higher speed. Additionally, the overall equipment and operating costs are generally lower, making it highly economical for bulk manufacturing. Thus, shops focused on high-volume structural output will find plasma systems exceptionally cost-effective.
Hybrid Approach: Using Both Technologies
Therefore, many fabrication shops find that CNC laser cutting and plasma cutting are complementary, not competitive. A common hybrid approach:
| Product Mix | Best Technology |
|---|---|
| Thin stringers (4-10mm) + standard profiles | Laser cutting |
| Thick stringers (12-25mm) + structural components | Plasma cutting |
| High-volume standard stringers | Laser cutting for speed and edge quality |
| Heavy-duty / custom / outdoor stringers | Plasma cutting for thickness and cost |
| Mixed production (thin + thick) | Both technologies |
Best Practices for High-Volume Production
For high-volume staircase stringers production, follow these best practices:
For CNC Laser Cutting:
- Use proper assist gas—nitrogen for clean stainless cuts, oxygen for mild steel
- Optimize laser pulse settings for material thickness
- Maintain clean material—remove rust or scale
- Invest in nesting software—maximize material utilization
- Use 6-15kW fiber lasers for 4-15mm steel
For Plasma Cutting:
- Choose appropriate amperage—higher current for thicker material
- Maintain consumables—replace electrodes and nozzles regularly
- Set correct torch height—standoff distance affects cut quality
- Use water table or downdraft—control fumes
- Budget for post-processing—grinding or deburring for weld prep
Quality Control Comparison
Quality control ensures every cut meets specifications. Here’s how to inspect laser and plasma cuts:
| QC Check | Découpe au laser | Plasma Cutting |
|---|---|---|
| Dimensional accuracy | Laser measurement | Caliper measurement |
| Edge quality | Visual—no slag | Visual—check for dross |
| Heat-affected zone | Minimal | Check for edge hardening |
| Consumable condition | Monitor power output | Check electrodes/nozzles regularly |
Why Choose Meizstairs for Your Cutting Technology?
We are a custom staircase manufacturer with 15 years of experience in steel stair fabrication—utilizing the right cutting technology for every project.
| Category | Details |
|---|---|
| Cutting technology | CNC fiber laser (thin materials), CNC plasma (thick/heavy materials) |
| Materials | Carbon steel (S275, S355), stainless steel |
| Stair types | Straight stairs, L-shaped stairs, U-shaped staircase, curved stairs, mono stringer stairs, spiral stairs |
| Applications | Home stairs, residential stair, commercial staircase, custom steel stairs |
| Certifications | IRC-compliant, IBC-compliant |
Free services:
- Cutting technology assessment—we recommend laser or plasma for your project
- Nesting optimization—maximize material utilization
- Post-processing guidance
Final Checklist Before You Choose Your Cutting Technology
- Have you identified your typical material thickness range?
- Have you calculated your production volume?
- Have you considered post-processing requirements?
- Have you budgeted for consumables and maintenance?
- Have you evaluated both capital and operating costs?
- Have you considered the types of staircase stringers you produce most often?
- Have you accounted for material condition (rust, scale, paint)?
- Have you planned for future production needs?
Technical Summary: Choosing between CNC laser and plasma cutting for staircase stringers production requires evaluating four key dimensions. First, consider material thickness—laser excels at 4-10mm, plasma dominates at 12mm+. Next, assess production volume—high-volume thin parts favor laser speed, while thick structural components favor plasma cost-effectiveness. Then, evaluate edge quality requirements—laser delivers burr-free edges with minimal heat-affected zone, plasma may require post-processing. Finally, analyze capital and operating costs—laser has higher upfront cost but lower consumable costs, plasma offers lower entry cost with higher consumable usage. As a result, the optimal cutting technology for staircase stringers production depends on your specific material mix, production volume, and quality requirements—and many shops benefit from a hybrid approach using both technologies.
Ready to Choose Your Cutting Technology?
With these factors in mind, you’re ready to make an informed decision. Contact Meizstairs today. We will help you assess your production needs and recommend the optimal cutting technology for your staircase stringers fabrication.